

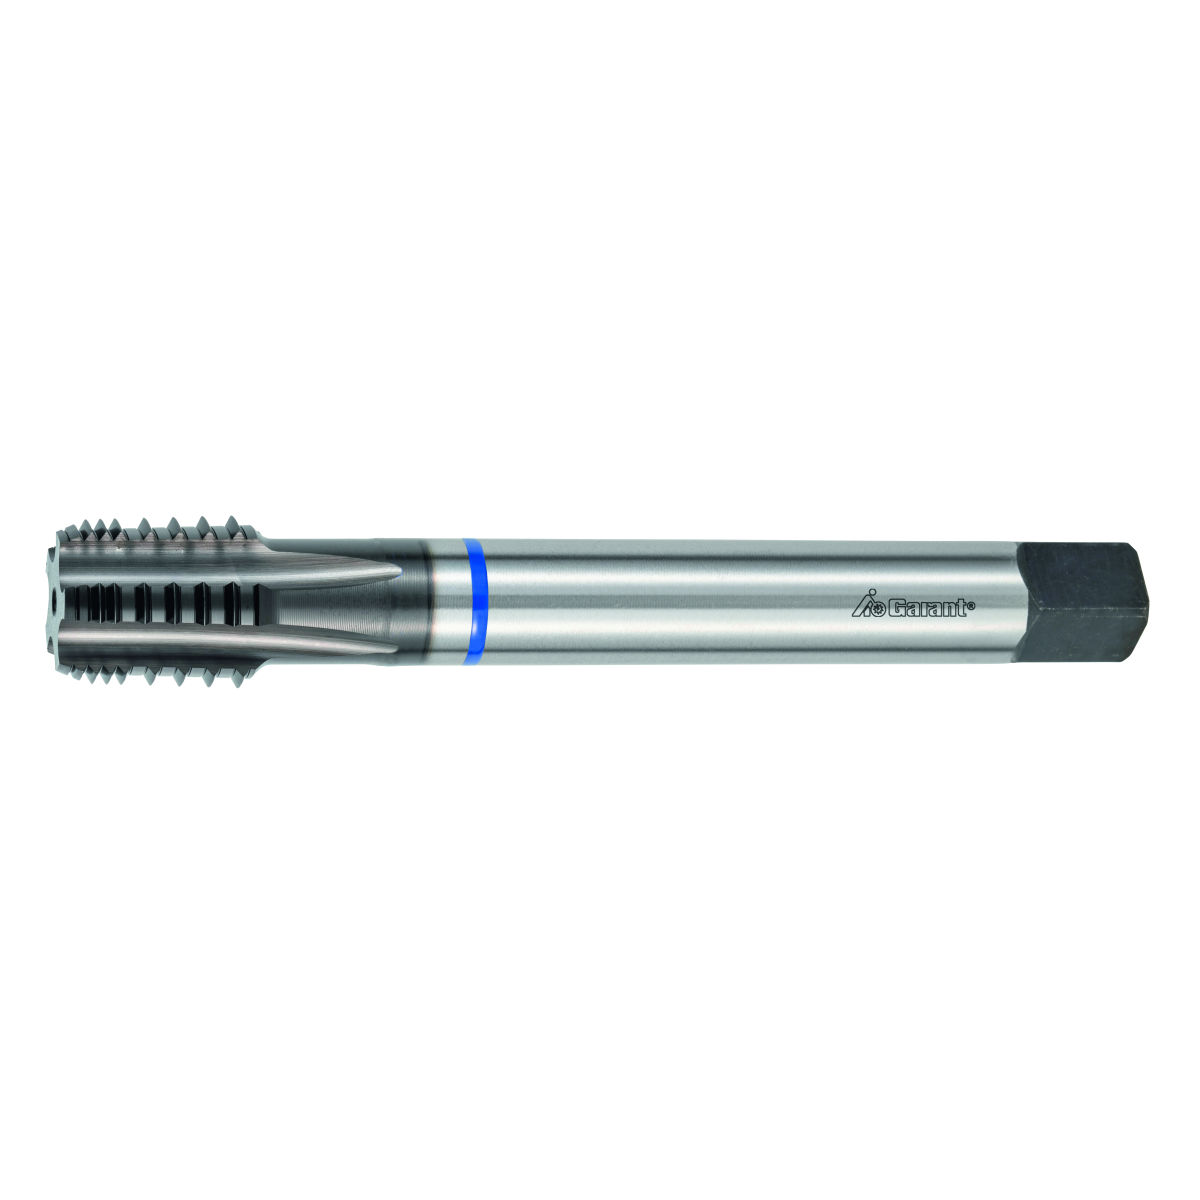


{{ name }}
Article no. {{ combinedCodeWithHighlight }}
Article code:
EAN / GTIN:
Manufacturer number:
Cat. No.:

| Through-coolant | no | |
| Cooling lubricant | yes | |
| Interface position | on the machine | |
| Holder type | plain shank | |
| Interface coding | ZYL02502105 | |
| Arbor size | 0250 | |
| Shank diameter DS | 25 mm | |
| Length of shank LS | 116 mm | |
| Thread type | NPT | |
| Cutter diameter D | 33.228 mm | |
| Nominal diameter of metric thread D | 31.745 mm | |
| Nominal diameter of inch thread D | 1 in | |
| Thread D | 1-11,5 NPT | |
| Thread pitch | 2.209 mm | |
| Turns per inch | 11.5 | |
| Chisel edge diameter | 28.32 mm | |
| Length of tapping part Lc | 34.61 mm | |
| Tap infeed length | 4.42 mm | |
| Taper lead angle | 23 degrees | |
| Number of teeth | 5 | |
| Twist direction | neutral, straight | |
| Twist angle | 0 degrees | |
| Taper ratio | 1:16 | |
| Type of thread-cutting tool | machine tap for conventional machining | |
| Taper lead form | C | |
| Application for type of drilling | through hole; blind hole | |
| Number of clamping slots | 5 | |
| Core hole diameter | 28.6 mm; 29 mm | |
| Tapping hole minimum depth | 27.4 mm | |
| Flank angle | 60 degrees | |
| Micrometer standard | yes | |
| Maximum check gauge diameter | 29.69 mm | |
| Check dimension tolerance | 0.05 | |
| Square-drive width across flats □ | 20 mm | |
| Tool material | HSS-E | |
| Cutting media, manufacturer’s designation | HSSE TIALN | |
| Coating | TiAlN | |
| Interface | joint 1 | |
| Gauge length A | 170 mm | |
| Usable length L1 | 58 mm | |
| Overall length L | 170 mm | |
| Weight | 772 g | |
| Cutting direction | right-hand cutting | |
| Standard | DIN 374 | |
| Machining method | thread processing internal (EGI) | |
| Colour ring | blue | |
| Type of product | taps |
| Article number | 519865 | |
| Catalog number | 138110 | |
| EAN / GTIN | 4045197533715 | |
| Manufacturer number | 138110 1-11,5 | |
| Article class | 11H | |
| Manufacturer/responsible person | Hoffmann Supply Chain GmbH & Co. KG, Poststraße 15, 90471 Nürnberg, Germany, www.hoffmann-group.com |


